
Crankpin Repair Case Study: Heat-Cracked Crankshaft Restored On-Site
Client: Confidential
Industry: Power Generation
Location: Africa
Duration: Completed within days
Service: In-situ Crankshaft Grinding Service
Overview
Royce Onsite Machining was contracted to carry out an urgent in-situ crankpin repair following a significant engine failure on a power generation unit. Crankpin No. 6 exhibited visible surface damage, heat cracks, and excessive hardness readings of 600 Brinell — well beyond OEM operating limits.
To avoid a full crankshaft replacement and extended downtime, the client required a complete in-situ recovery. Our technicians were mobilised within days to assess, machine, heat-treat, and fully restore the crankpin — without removing the crankshaft from the engine block.
Work Carried Out
Crack Removal
- Initial proof machining exposed persistent cracking.
- MPI (Magnetic Particle Inspection) confirmed the presence of heat-induced surface cracks.
- Further machining and testing ensured complete crack elimination.
Heat Treatment (Annealing)
- The crankpin surface showed excessive hardness (600 Brinell).
- A 14-hour in-situ annealing process successfully reduced hardness to within OEM standards.
Crankshaft Straightening
- Run-out checks on adjacent journals revealed a shaft bend.
- After OEM consultation, we applied our specialist peening method, using multiple peening sessions to restore the shaft to correct alignment.
Redesign of Radii & Final Machining
- The OEM specified a new radii profile to accommodate the reduced pin diameter.
- We produced custom orbital tooling to match the revised specification.
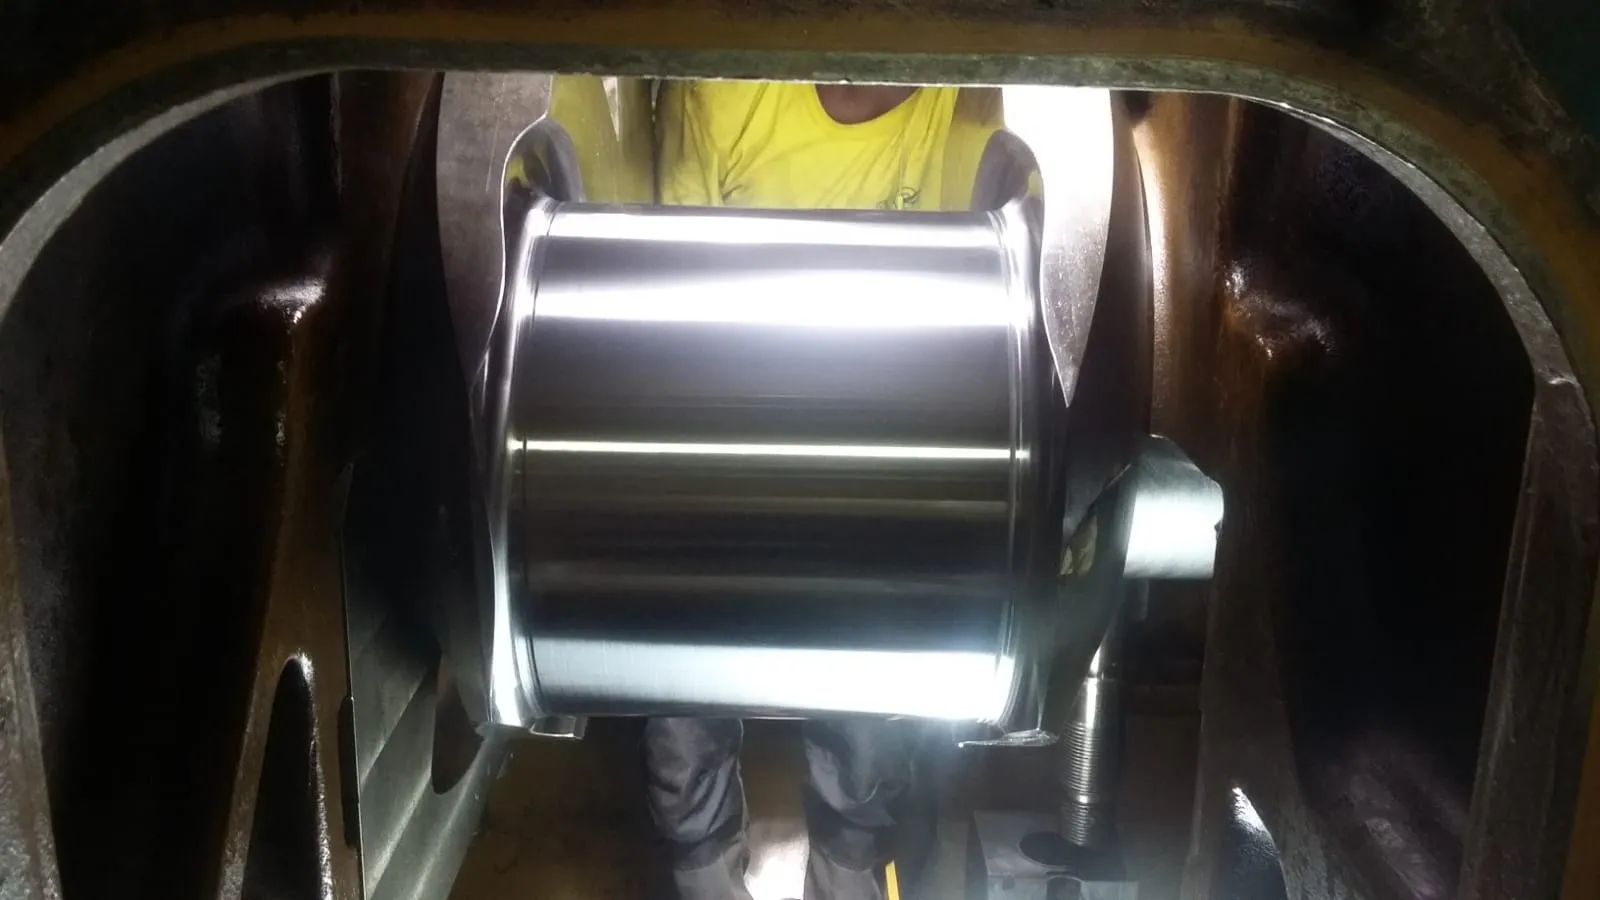
- Final machining brought Crankpin No. 6 to –3.00 mm undersize, followed by high-precision polishing.
Finishing
- Because of the exceptional finish achieved, the client requested polishing of all remaining crankpins to ensure consistent bearing-surface quality throughout the engine.
Technical Highlights
- Crankpin Final Size: –3.00 mm undersize
- Original Hardness: 600 Brinell
- Post-Annealing Hardness: Within OEM limits
- Flatness Restored: 98%
- Surface Finish Achieved: 0.2 Ra
- Run-Out Correction: Completed using in-situ peening method
Outcome
The full repair was completed in-situ within days, avoiding disassembly, shipping, and replacement delays. The engine was successfully reassembled, load-tested, and returned to full operational condition.
This project demonstrates Royce Onsite Machining’s ability to deliver OEM-standard repairs under challenging field conditions, significantly reducing downtime, cost, and risk.